Önerilen Ekipman
Eşleştirilmiş Ekipman
Metal tozdan pelet ekstrüzyona ve hassas CNC'ye — bu makineler modern kalıp iş akışının her aşamasını kapsar.
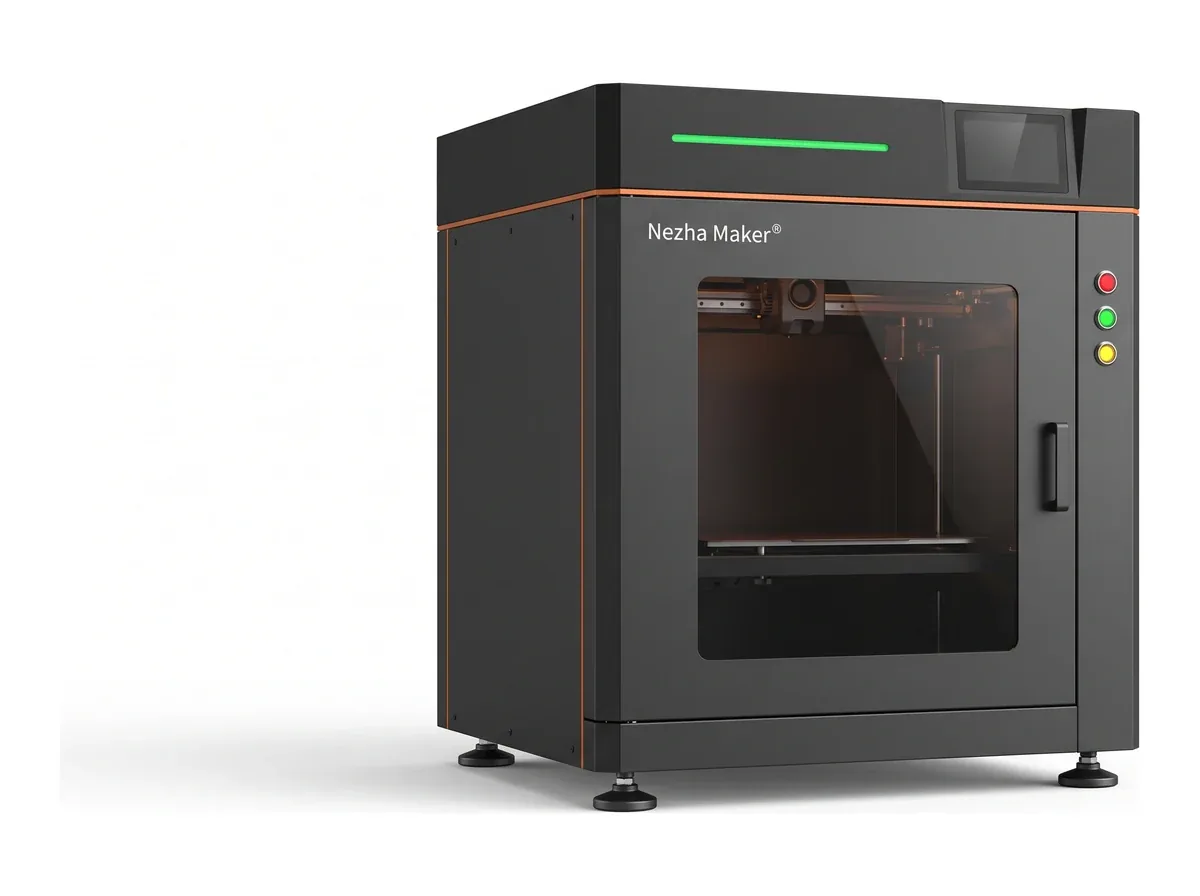
NZ-FGF-800H
Same build volume as NZ-FGF-800, specified for high temperature: heated chamber to 100°C, 450°C nozzle, 25kg dryer and pneumatic feeding. CNC motion controller for 7×24 running; absolute-encoder servos for power-loss resume.
Baskı: 800×600×800mm · hazne 100°C · PPS-CF / PA-CF
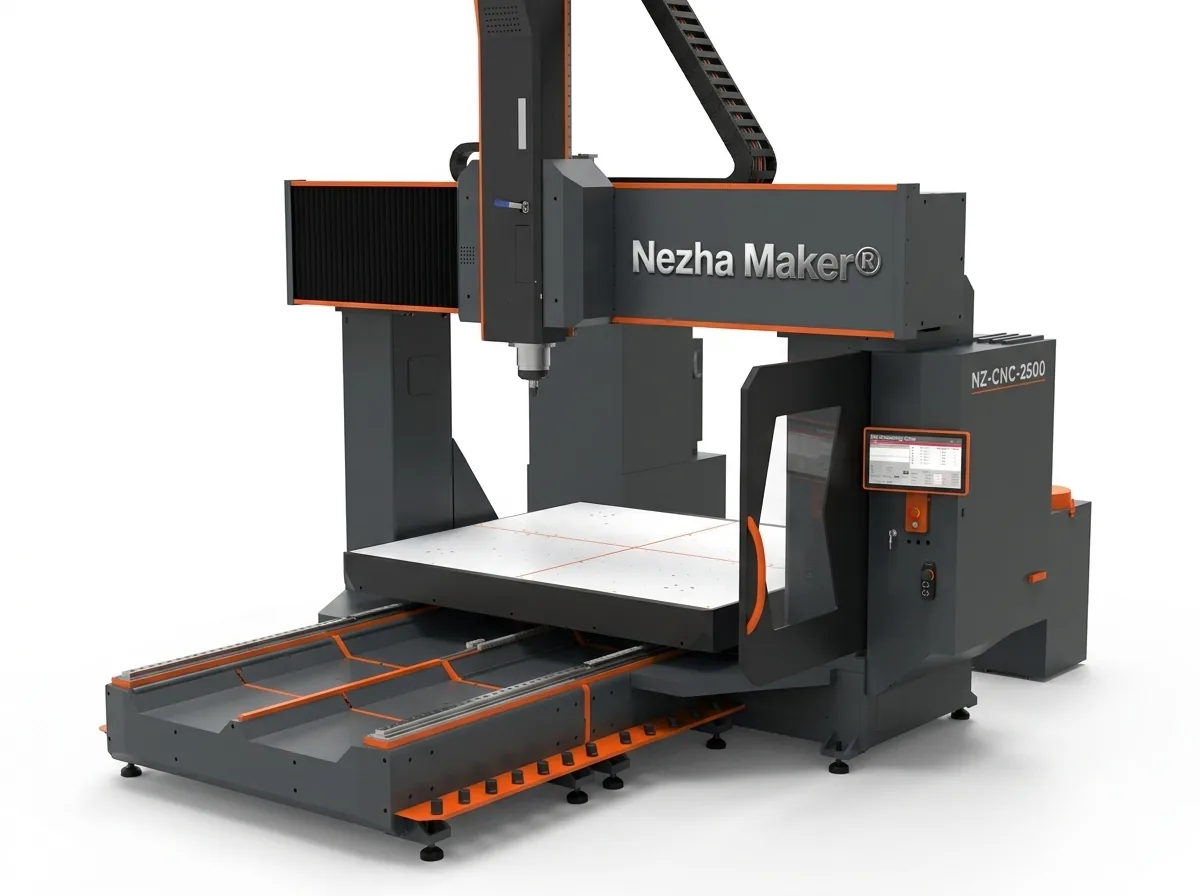
NZ-FGF-2400
Büyük polimer-kompozit pelet yazıcı — 2400mm hareket, yüksek akışlı vida (≤10kg/s). 4 metrelik heykeller, otomotiv master kalıpları, GFRP ikameleri.
Build: 2400mm class · up to 10kg/h
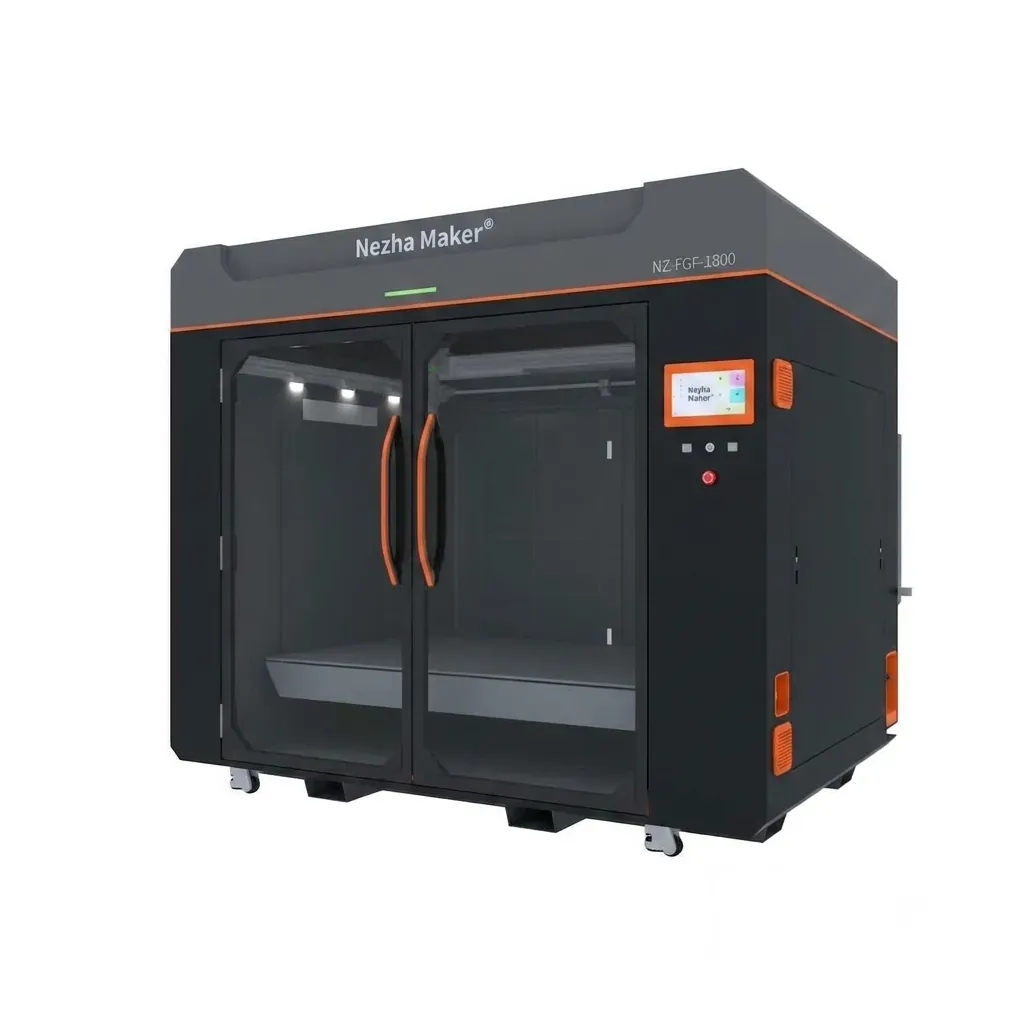
NZ-FGF-1800
Orta-büyük FGF — 1800mm hareket, yüksek akışlı vida ekstrüzyon; büyük heykeller, vitrin gereçleri, master kalıplar.
Build: 1800mm class · high-flow screw
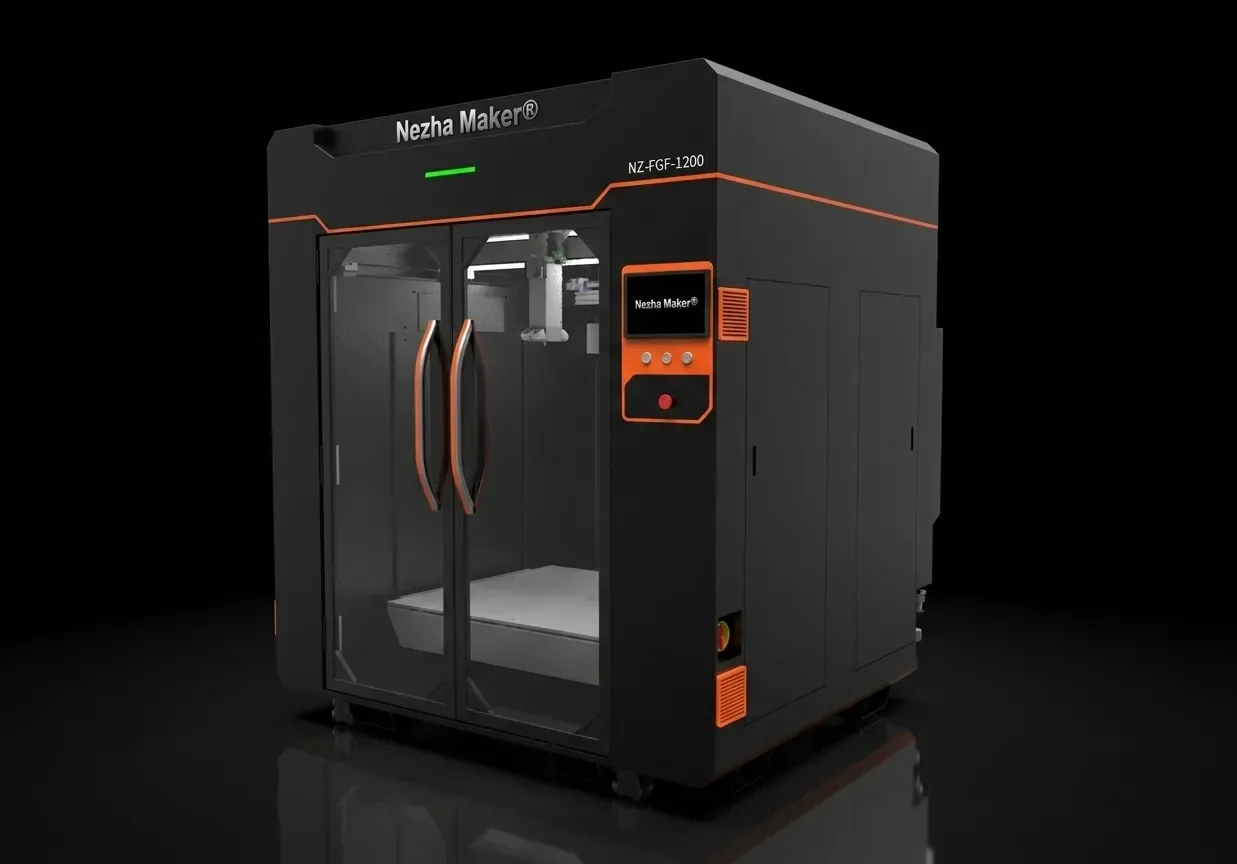
NZ-FGF-1200
Mid-size polymer-composite pellet printer — 1200×1000×1000mm, 1–8mm nozzle 3-zone heating, 40kg hopper integrated feeder, single-phase 220V, 950kg.
Build: 1200×1000×1000mm · 220V · PLA to PEEK+CF
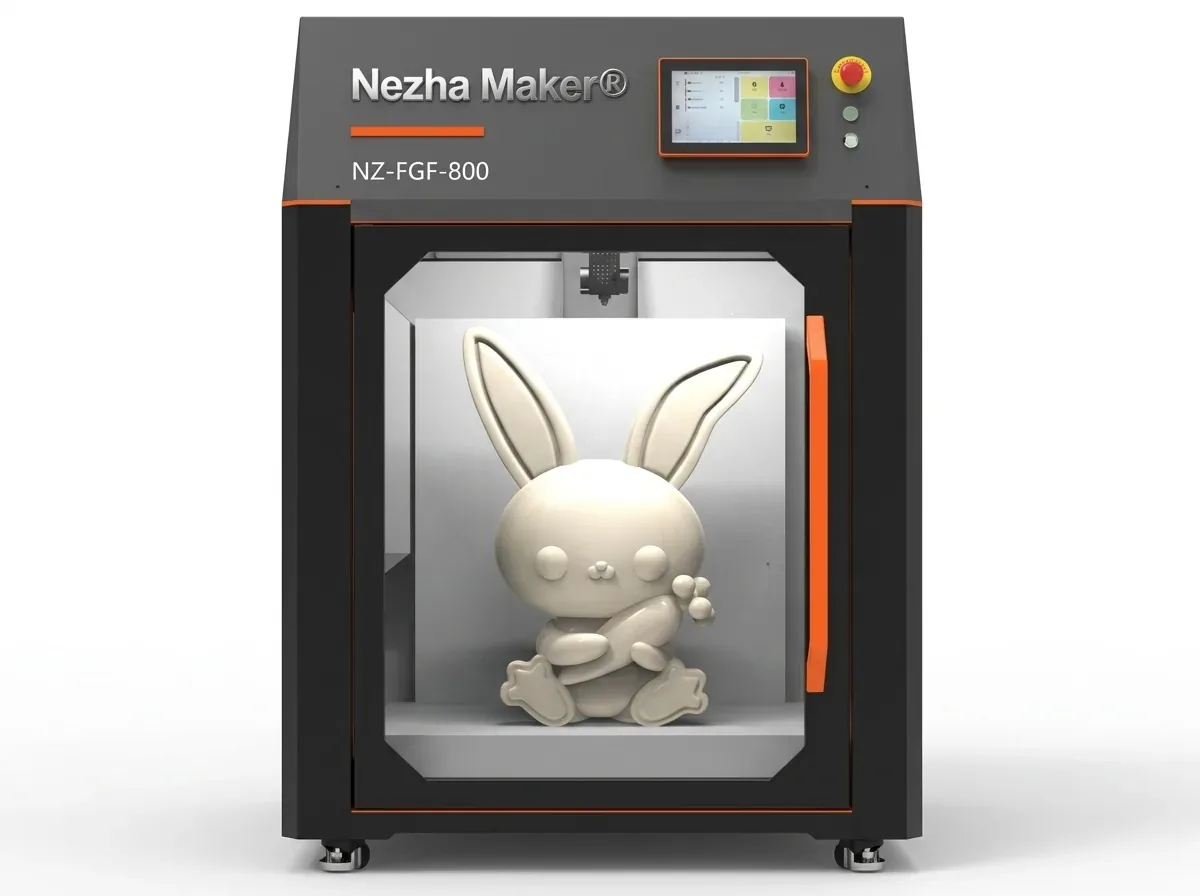
NZ-FGF-800
Polymer-composite pellet printer — 800×600×800mm, 0.4–3mm nozzle, 2-zone heating, 12kg hopper, optional chamber heating. General-purpose for PLA to PEEK+CF.
Build: 800×600×800mm · PLA to PEEK+CF pellets
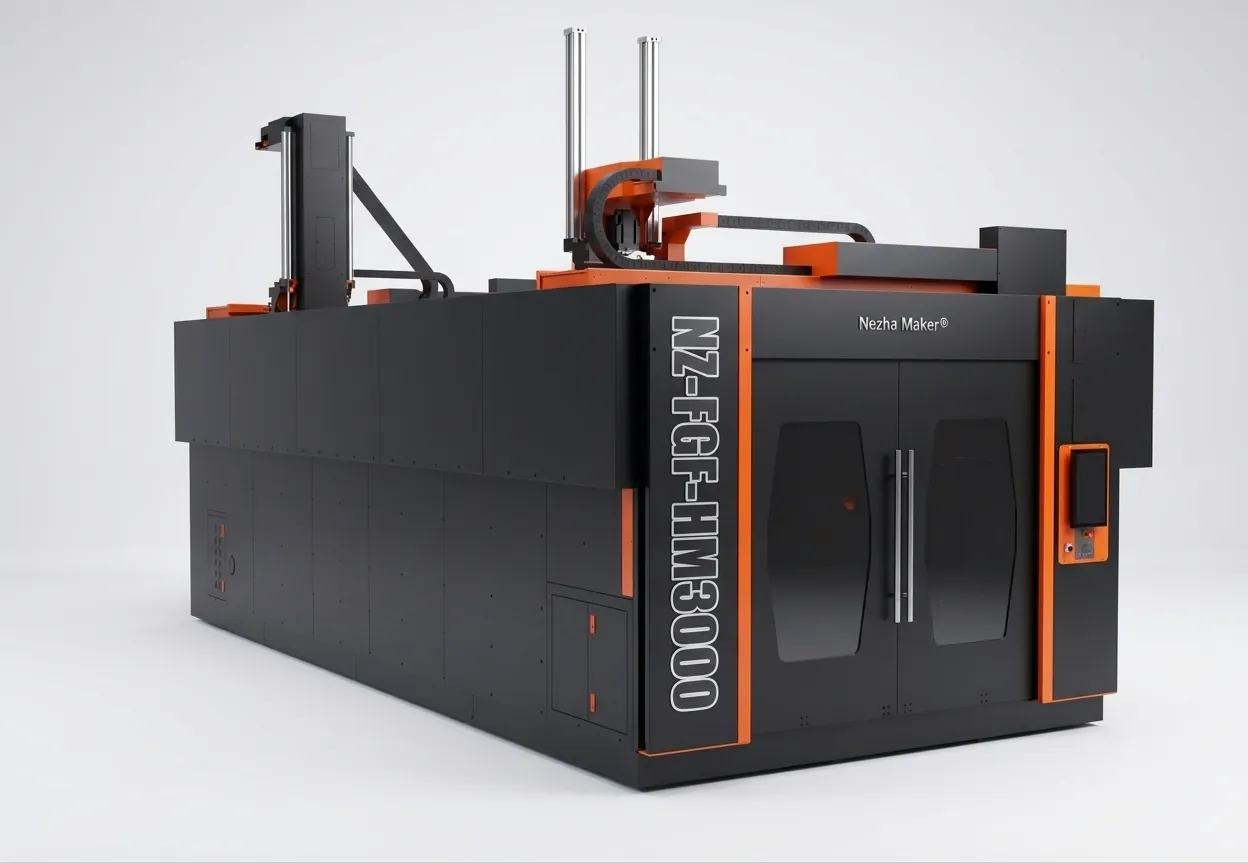
NZ-FGF-HM3000
Large polymer-composite additive+subtractive machine — 3000×2000×1000mm build & mill, 4–12mm nozzle 4-zone heating, 30kg/h max flow, 200kg tri-feeder, zoned aluminum bed ≤120°C, 70kW.
Build: 3000×2000×1000mm · up to 30kg/h · hybrid
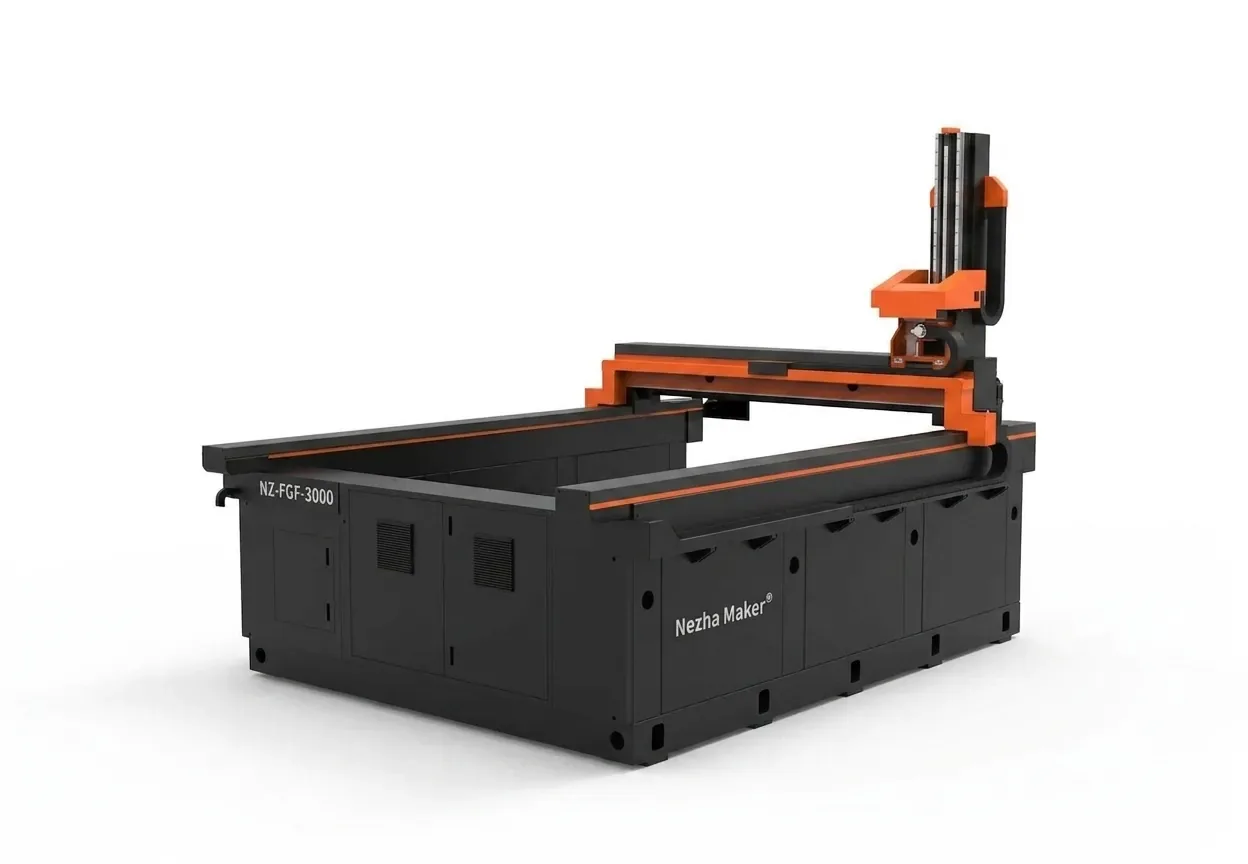
NZ-FGF-3000
FGF pellet 3D mold-printing machine — screw-extruded composite pellets print large industrial molds, 3000×2000×1000mm build, integrated dual-unit 100kg feeder, 6000kg.
Build: 3000×2000×1000mm · 6000kg · industrial molds
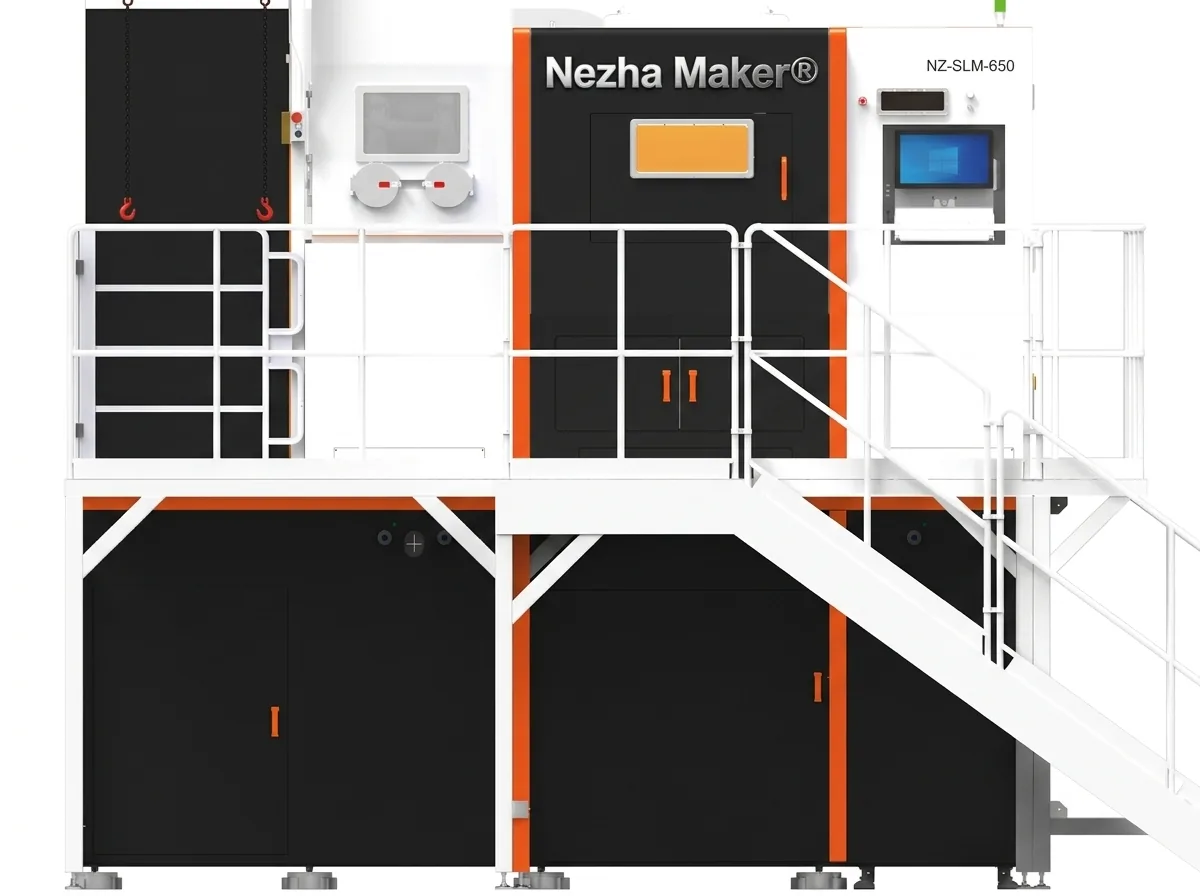
NZ-Metal-650
Dört lazerli aynı formatlı büyük metal yazıcı — 625×625×1100mm baskı, 7×24 saat denetimsiz otomatik toz besleme, 3× verimlilik.
Build: 625×625×1100mm · 4 lasers · SLM