Recommended Equipment
Matched Equipment
From high-precision resin pattern printers to large-format FDM for sacrificial prototypes — the full investment-casting workflow.
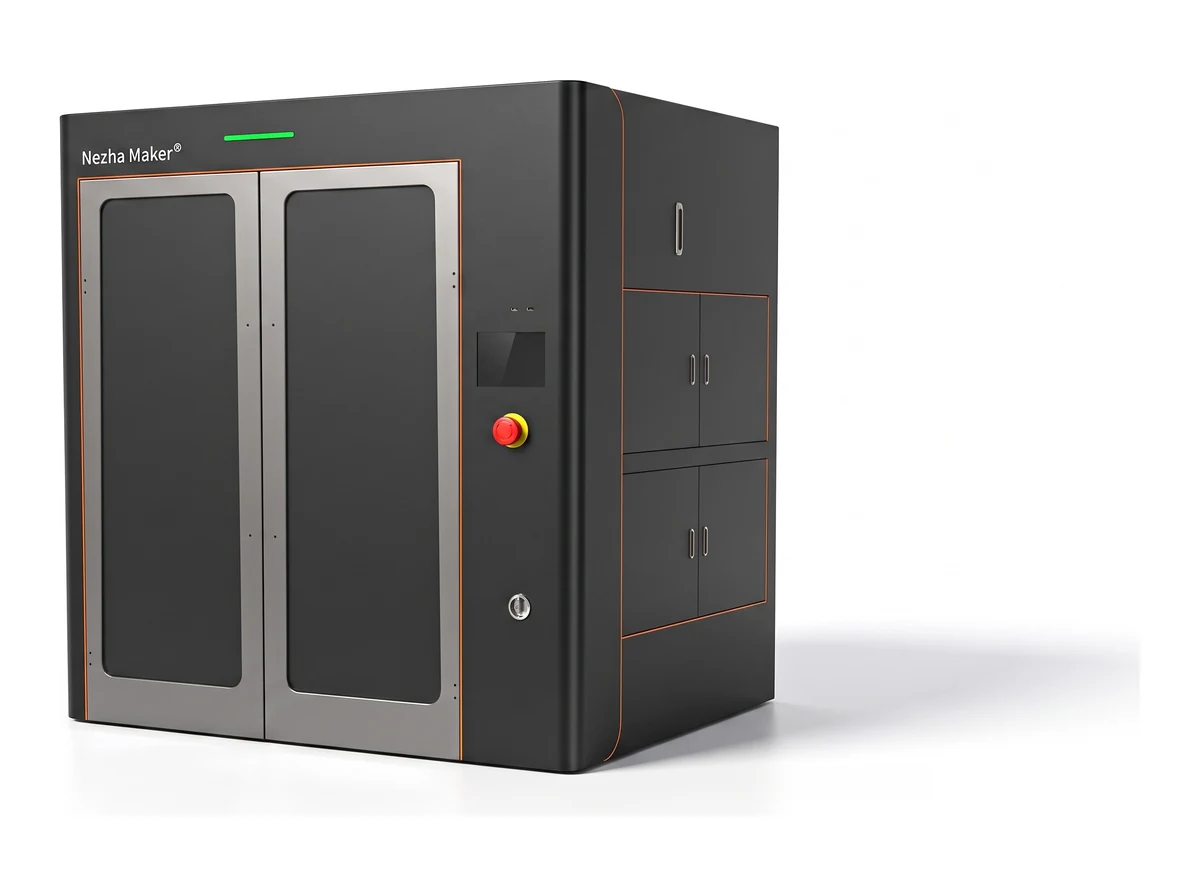
NZ-FDM-M1000 Pro
Industrial 1-meter FDM, CNC motion controller for 7×24 continuous running, new high-flow 1.75mm extruder (100% faster on ABS), non-contact laser levelling ±0.03mm over 400 points in ≤5min, absolute-encoder servos on all axes for true power-loss resume.
Build: 1 m class · 24/7 rated · power-loss resume
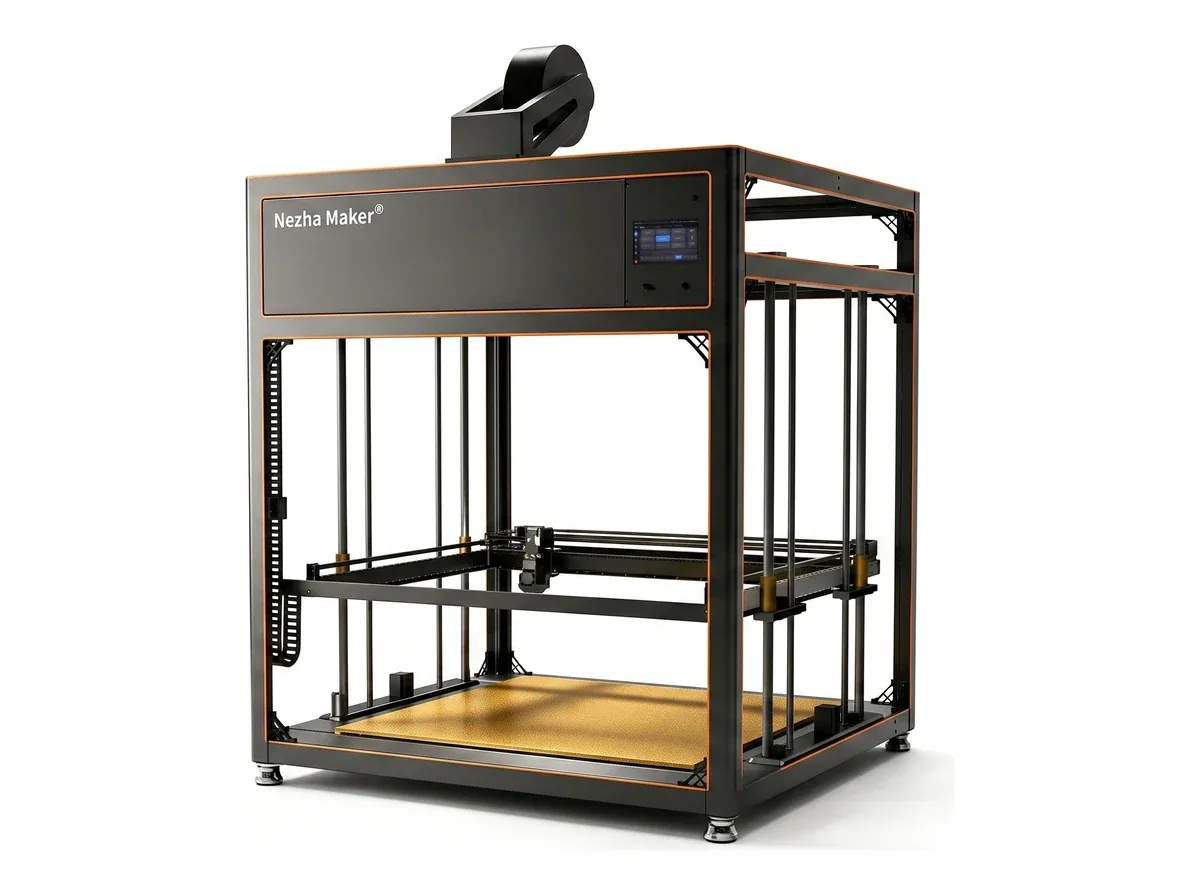
NZ-FDM-K1000
Meter-scale open-frame FDM: 3.5mm coarse filament, high-flow extruder reaching 300°C in 2 min at 100mm³/s+, CoreXY up to 500mm/s, fixed build platform. For sculpture, full-size automotive prototypes, foundry patterns.
Build: 1 m class · 100mm³/s+ · CoreXY 500mm/s
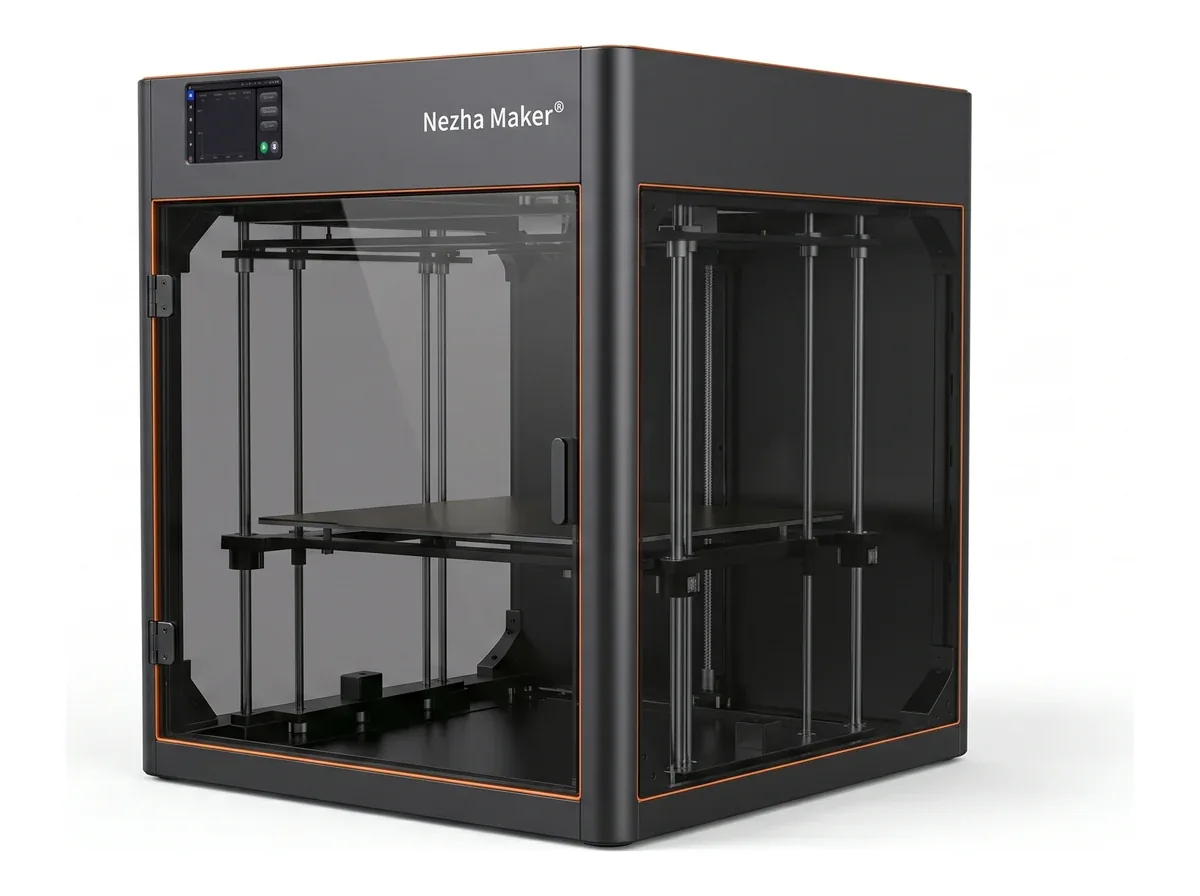
NZ-FDM-M500
Fully enclosed 500mm high-speed FDM. Klipper firmware at up to 600mm/s, CoreXY with closed-loop servos, four-screw four-rail Z, HGX V2 hardened-steel geared direct extruder, piezo auto-levelling.
Build: 500mm · Klipper 600mm/s · enclosed
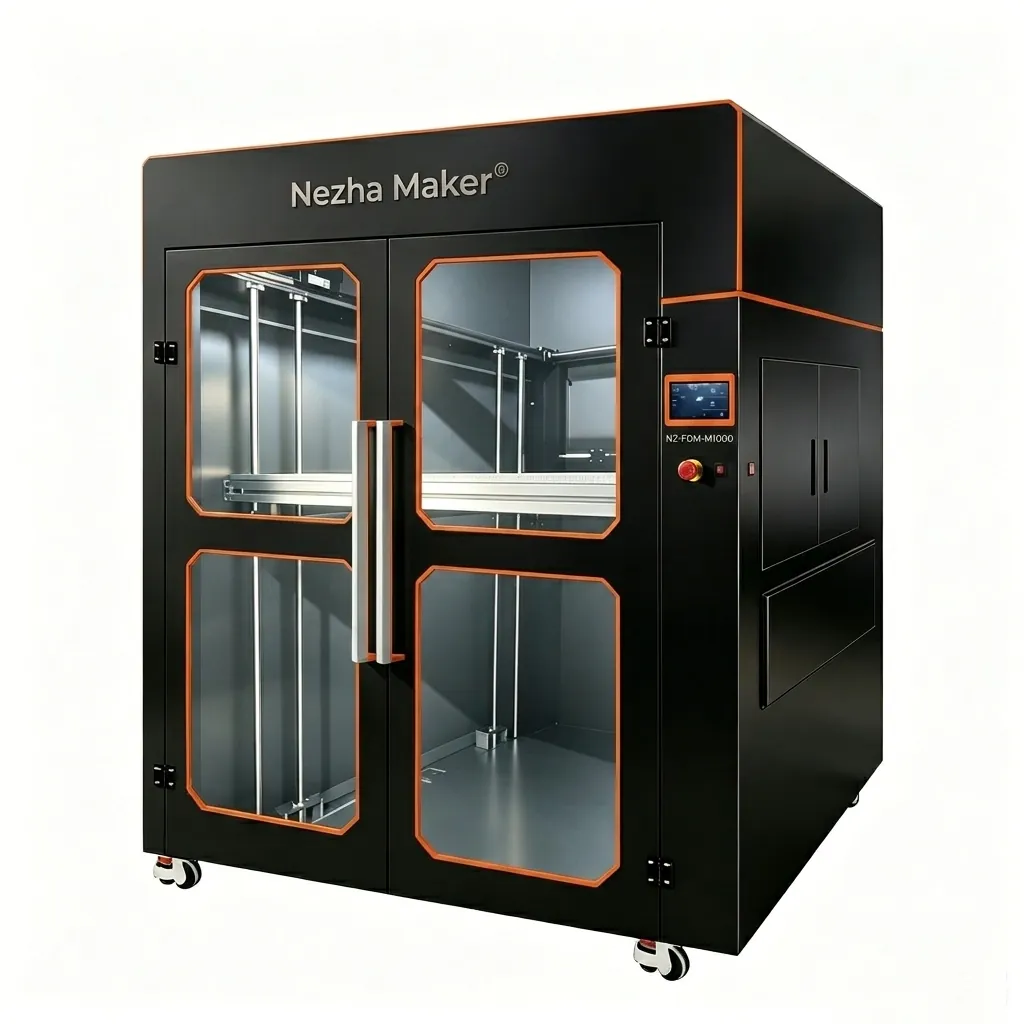
NZ-FDM-M1000 (1.75)
1-meter industrial FDM — silicone heated bed + 12mm aluminum plate, BMG dual-gear feed, 320°C hotend, dual-Z quad-axis screws. Built for fixtures, molds and large parts.
Build: 1 m class · nozzle up to 320°C
NZ-FDM-M1000 (3.5)
1-meter sculpture FDM — 3.5mm filament, 0.8–2.0mm nozzles, for large cultural sculptures & commercial display pieces.
Build: 1 m class · 3.5mm filament · 0.8–2.0mm nozzles
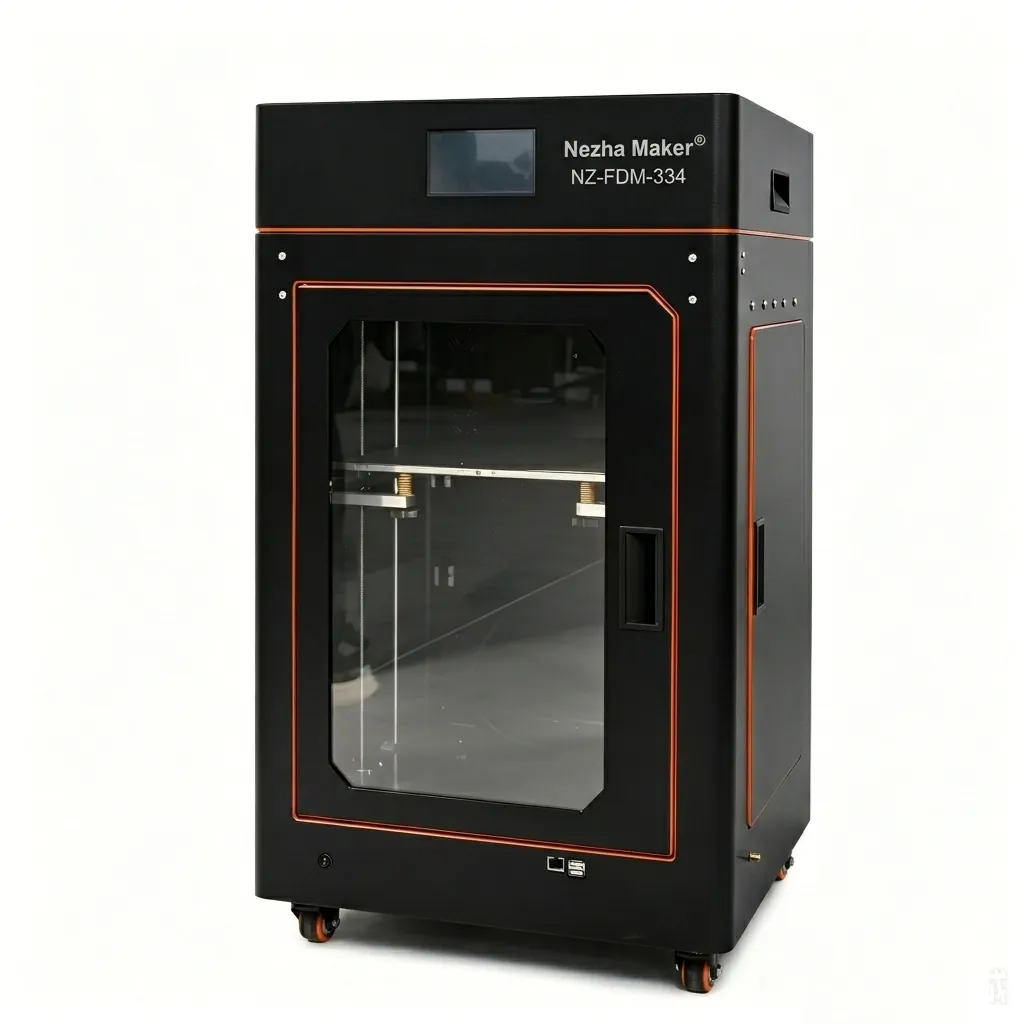
NZ-PEEK334
450°C high-temp FDM — 450°C hotend / 120°C bed / 60°C chamber, 0.0011mm XY accuracy. Prints PEEK for aerospace, medical and research.
Extruder up to 450°C · PEEK certified
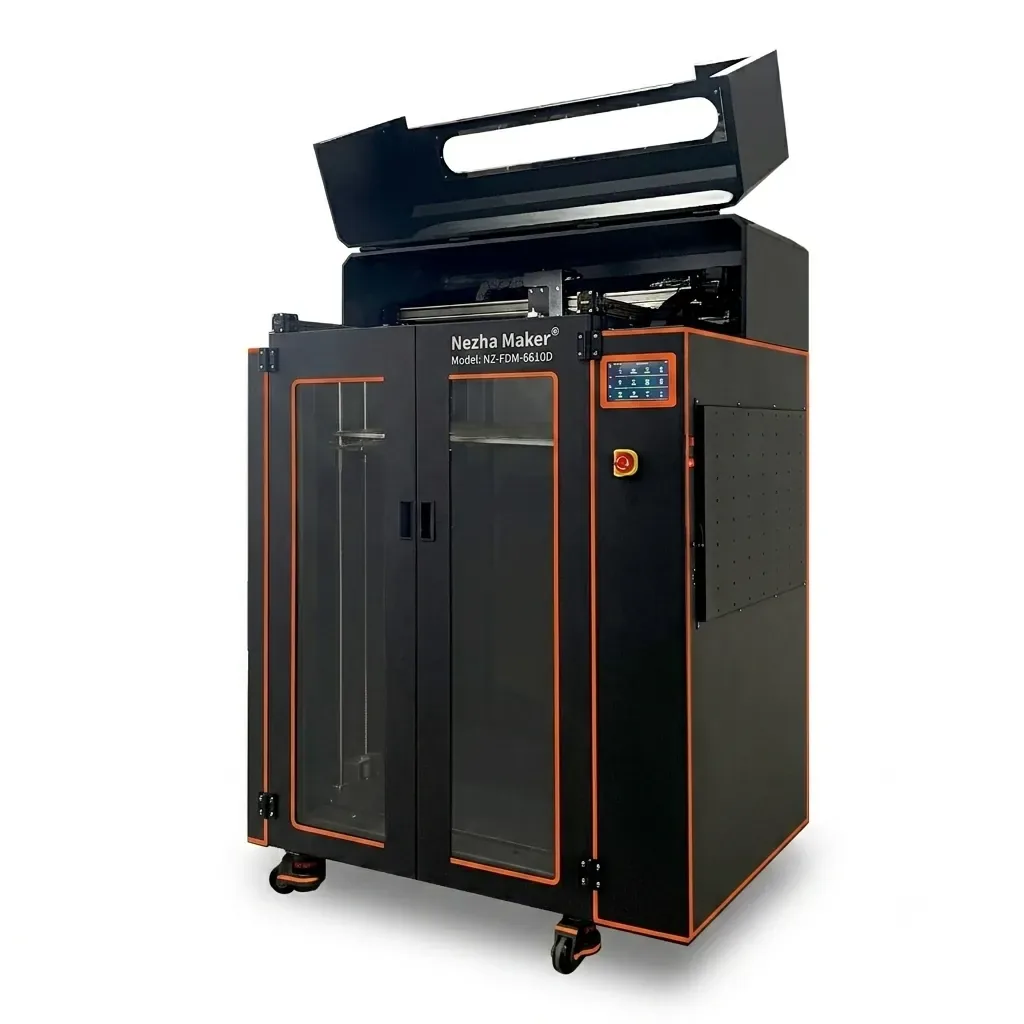
NZ-FDM-6610D
Large industrial FDM — 720h continuous, filament/power-loss recovery, custom even-heating nozzle, dual-door for large models.
720h continuous · dual-door · large models
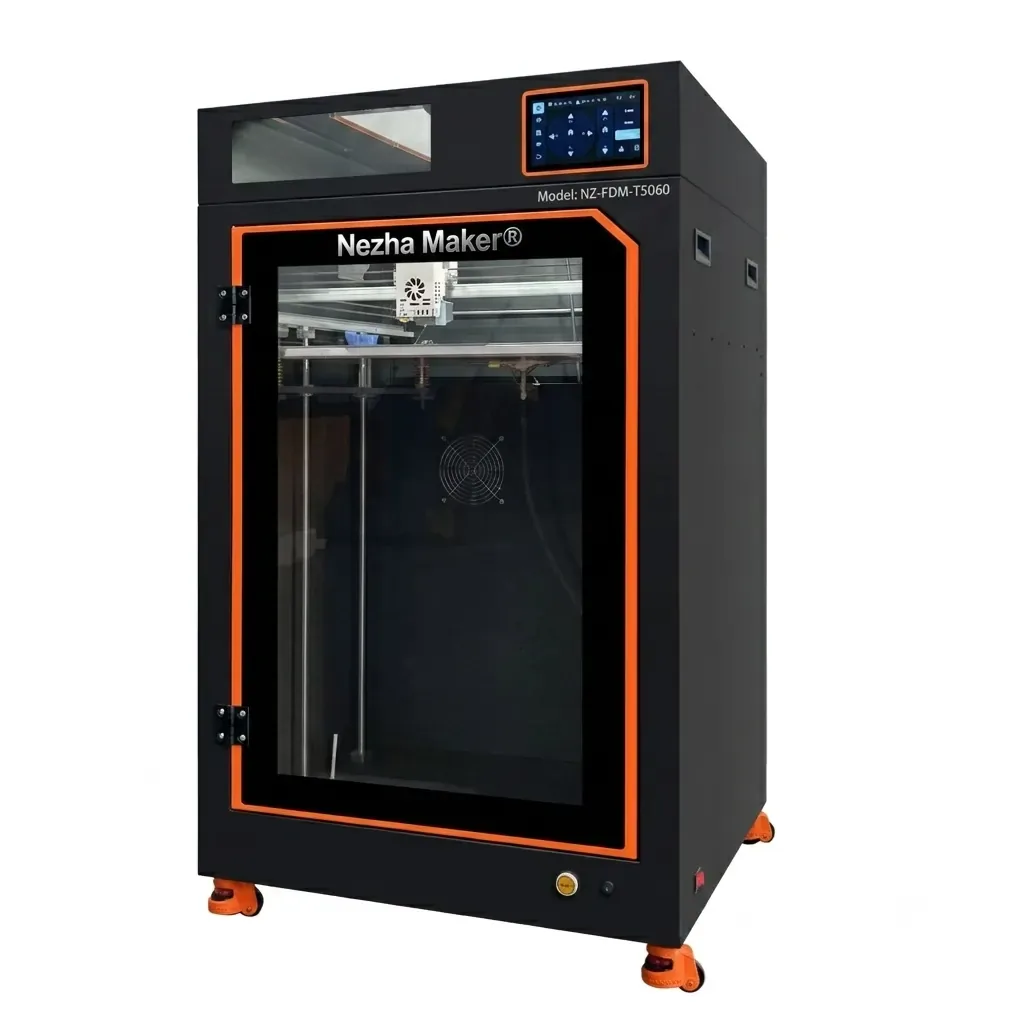
NZ-FDM-T5060
High-speed enclosed FDM — Klipper 600mm/s, 60°C thermal chamber for ABS/PETG/CF-nylon.
Klipper 600mm/s · 60°C chamber · enclosed